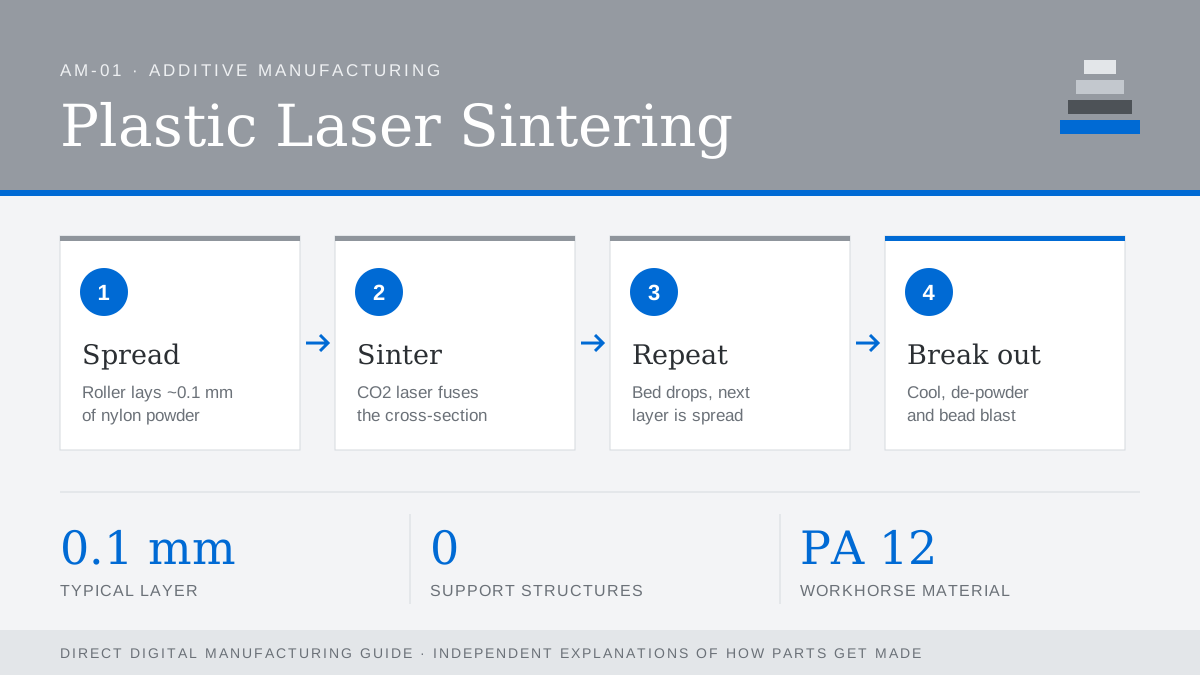
Plastic laser sintering, usually called selective laser sintering (SLS), builds parts from a bed of fine polymer powder. A roller spreads a layer roughly a tenth of a millimetre thick, a CO2 laser traces the part’s cross-section and fuses the particles, the platform drops, and the cycle repeats. The whole build chamber is held just below the polymer’s melting point, so each new layer bonds cleanly to the one beneath it.
Why engineers like it
- No supports. Unsintered powder holds the part in place, so overhangs, internal channels and interlocking assemblies print as-is.
- Nesting. Parts can be stacked in three dimensions, making SLS efficient for batches of small components.
- Real mechanical properties. Nylon 12 and nylon 11 are tough, fatigue-resistant and chemically stable, good enough for many end-use parts.
Common materials
| Material | Character |
|---|---|
| PA 12 | The workhorse: balanced strength, good detail |
| PA 11 | More ductile and impact resistant, bio-based |
| Glass- or carbon-filled PA | Stiffer, more heat resistant, slightly brittle |
| TPU | Rubber-like flexibility for seals and grips |
Design guidelines
- Keep walls at 0.8 mm or more; 1.5–2 mm gives sturdier parts.
- Add escape holes (at least 3–5 mm) to hollow sections so trapped powder can be removed.
- Expect a slightly grainy surface; bead blasting, dyeing or vapor smoothing improve it.
- Large flat plates can warp as they cool, so add ribs or orient them at an angle.
When to choose something else
If you need a glossy cosmetic finish or features under about half a millimetre, stereolithography is usually the better fit. If you need thousands of identical parts, the economics shift toward injection molding.